0+Shops Worldwide

  • Premium Chinese Carbide Rods
  • ±0.005mm Tolerance
  • Ships in 48 Hours
The Agony

Why Your Current Tools Are Costing You More Than Just Money

If you run a machine shop, you already know these headaches. We built QT Tools specifically to remove them.

  • Inconsistent Quality

    Tired of the first batch being great and the second batch breaking? Most low-cost mills hide recycled carbide. The grain structure swings from lot to lot — so your tool life becomes a gamble you can't quote a job around.

  • Coating Peeling

    Why do "premium" coatings fail after minutes? When pre-treatment is skipped, the coating never truly bonds. It peels, welds chips to the edge, ruins your finish, and wrecks your cycle time.

  • Supply Chain Lag

    Why wait 8 weeks for big brands while your machines sit idle? Factory-direct supply means fast response and stable lead times — so your spindle keeps turning and your competitor doesn't ship first.

The Science · The QT Standard

German quality, engineered in China

We don't just sell tools — we manage every micron of precision. Here is exactly what goes into a QT Tools end mill.

Module A — The Substrate

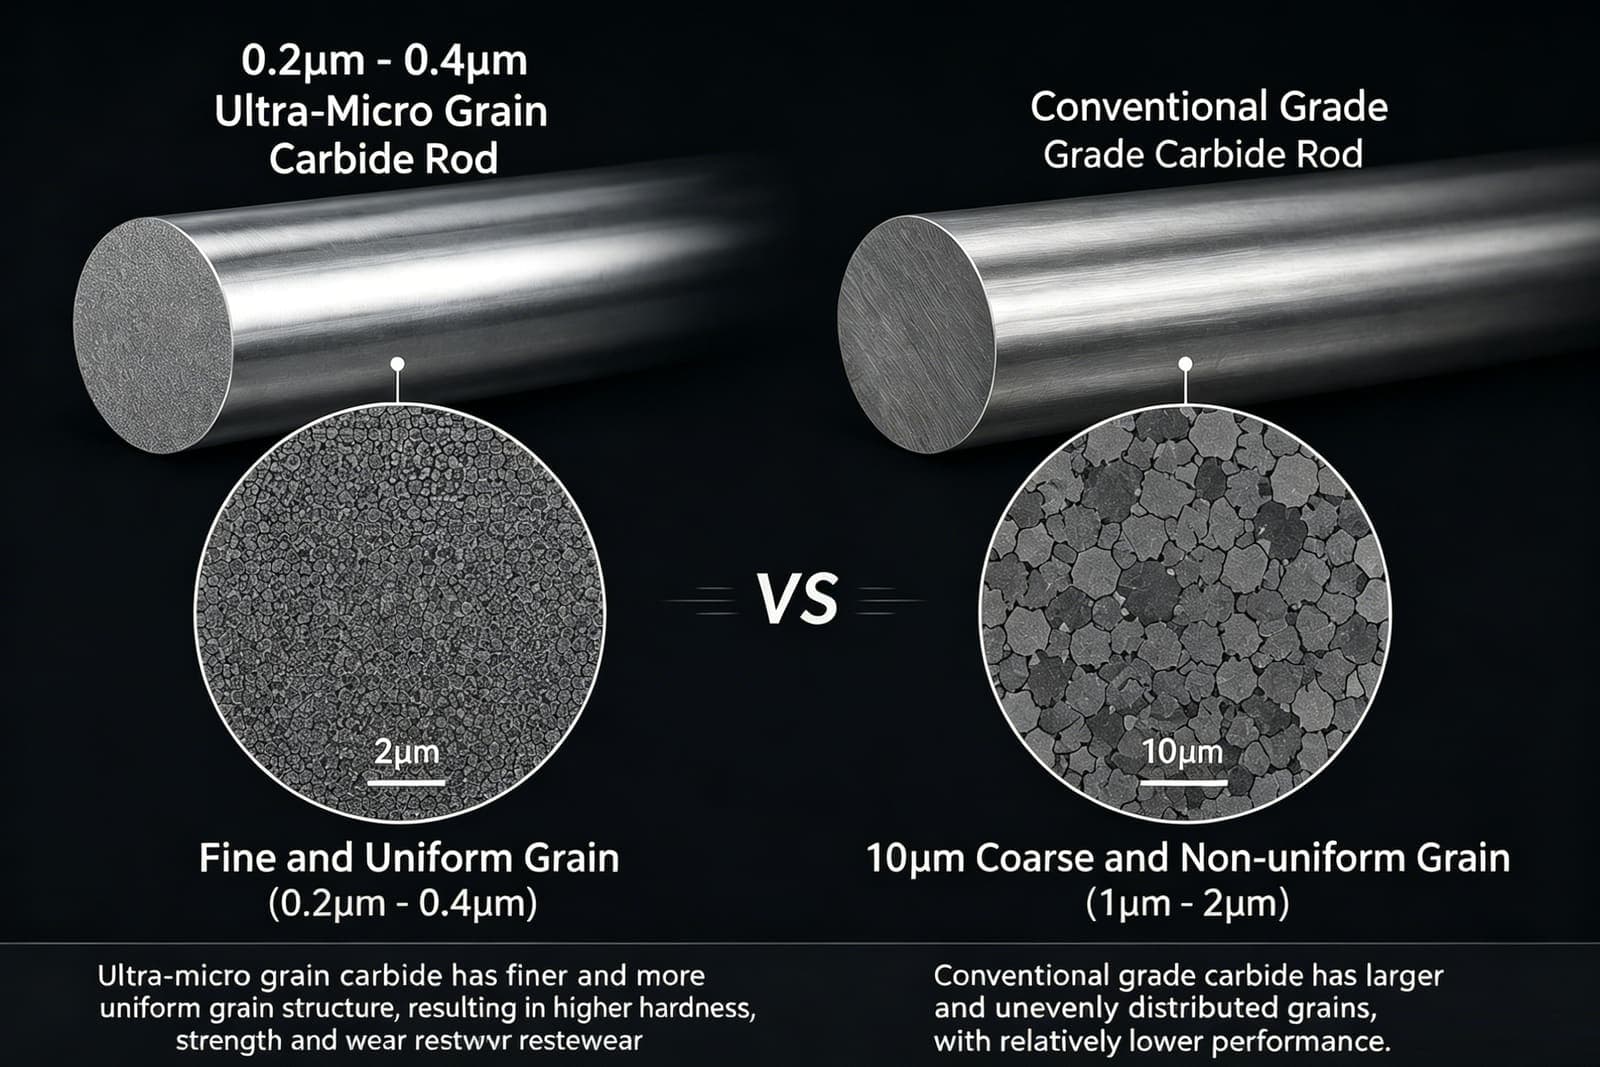
Ultra-micro grain carbide rod

We grind only from ultra-micro grain carbide rods, with a grain size of just 0.2μm–0.4μm. Finer grain means a sharper, stronger edge that resists chipping under heavy radial load — so your tool life stops being a gamble.

  • 0.2μm – 0.4μm ultra-micro grain
  • Premium imported rods
  • Higher transverse rupture strength
Get Free Technical Advice
Module B — The Coating

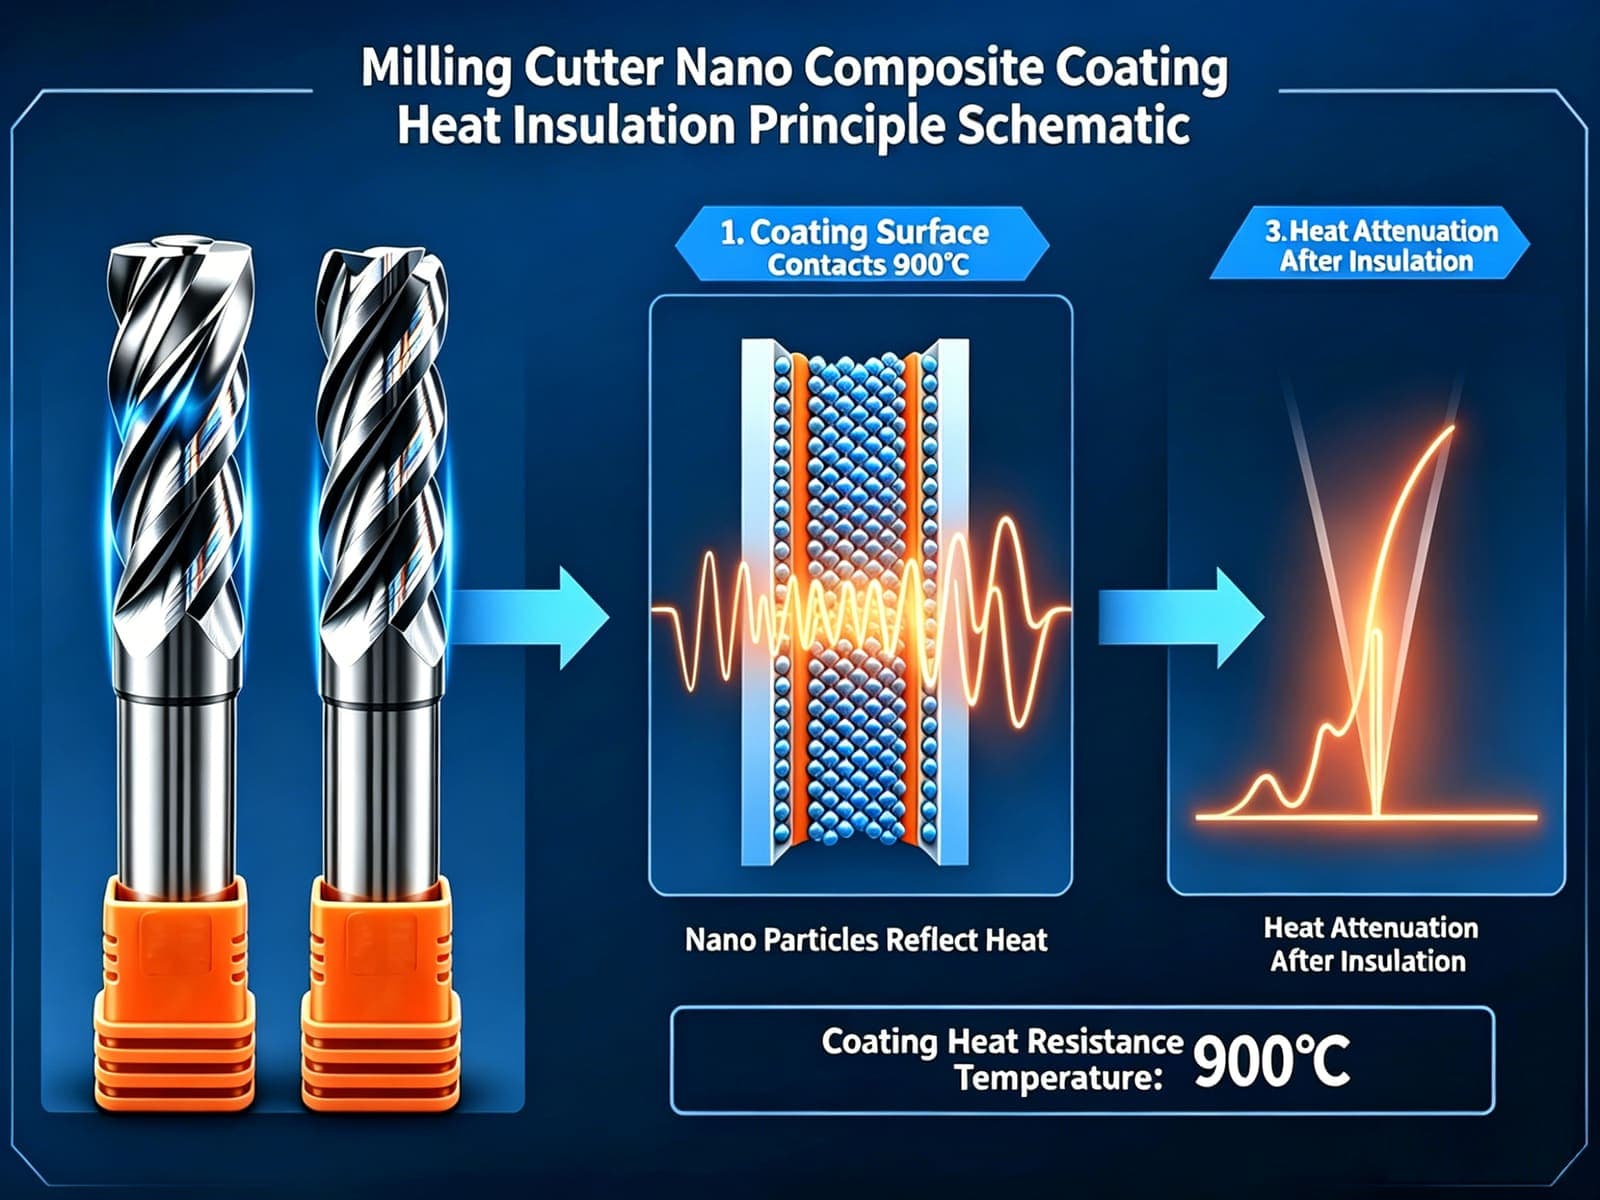
Nano-composite coating, stable to 900°C

Our nano-composite AlTiN / TiSiN coating forms a protective oxide layer at high temperature, exactly when your tool needs it most. The result: no chip welding, a cleaner finish, and heat resistance up to 900°C in dry, high-speed cutting.

  • Nano-composite AlTiN / TiSiN
  • Heat resistant up to 900°C
  • Anti-welding on hardened steel
Get Free Technical Advice
Module C — The Geometry

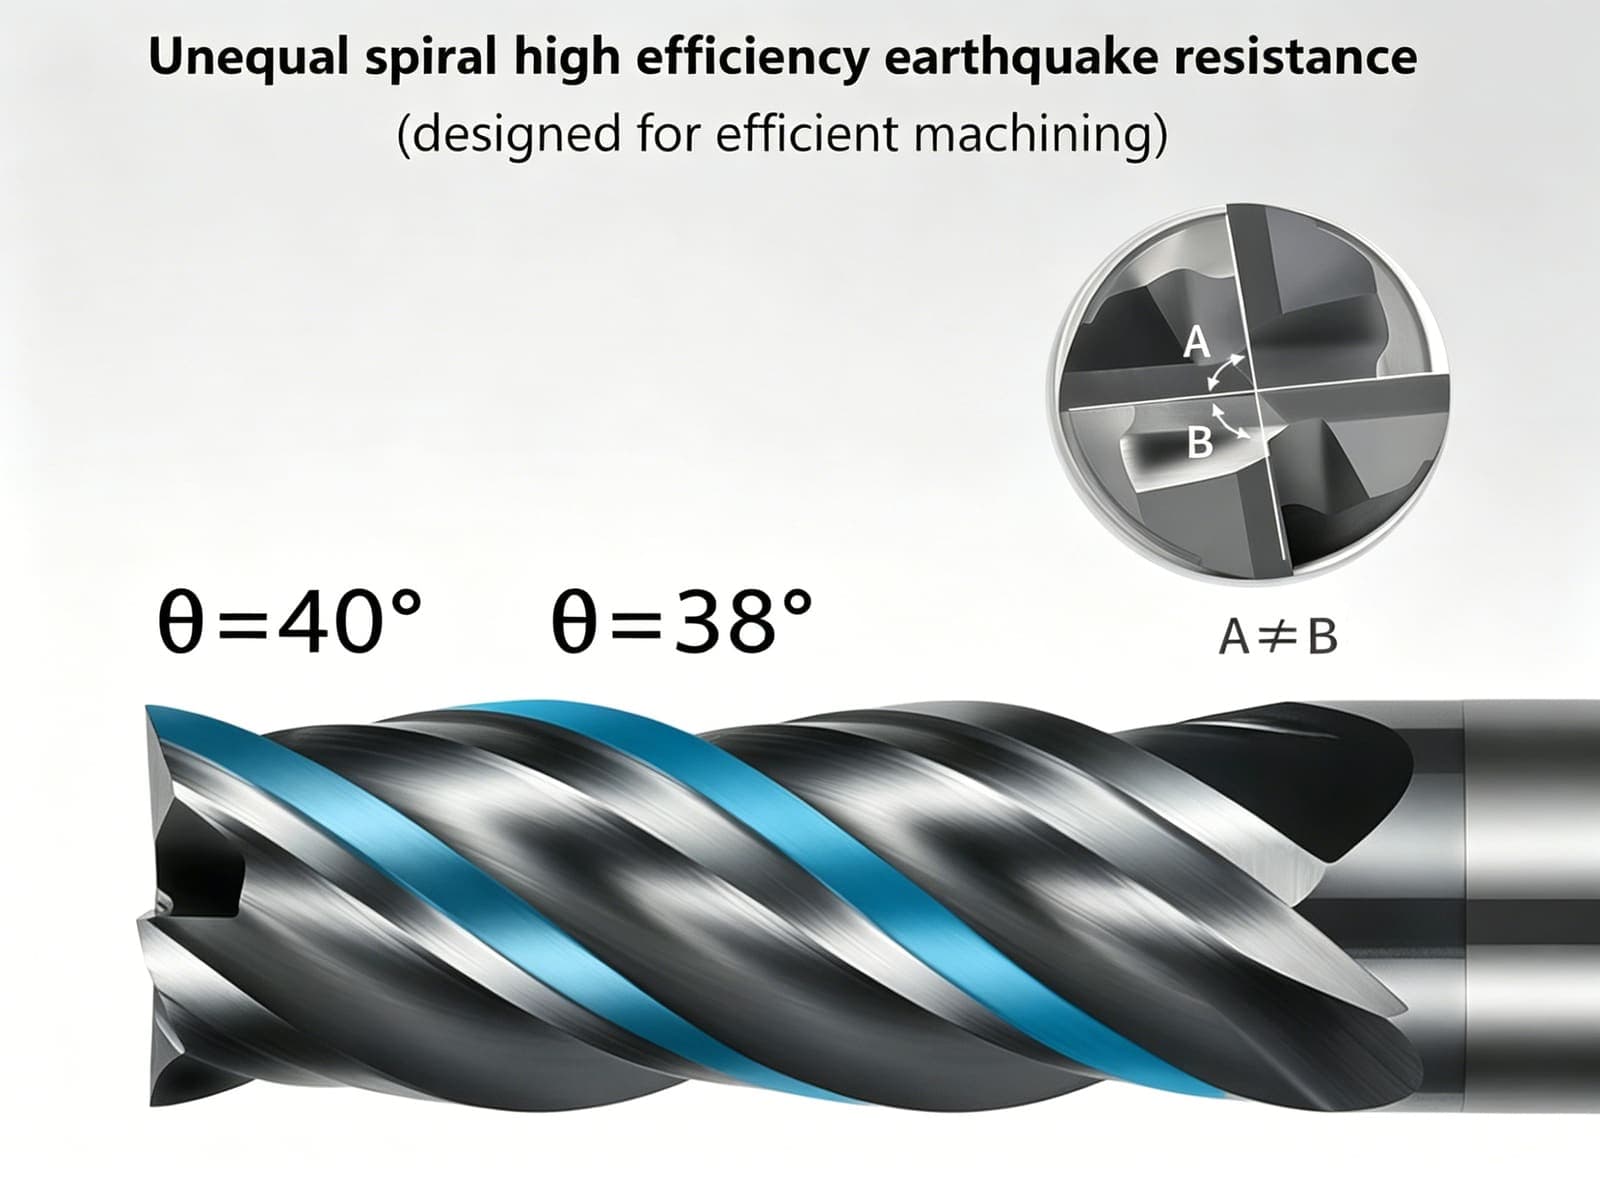
Unequal pitch helix kills chatter

Our unequal pitch (variable helix angle) design breaks up harmonic vibration like a silencer — suppressing chatter at high spindle speeds, protecting your machine, and letting you push higher feeds with confidence.

  • Unequal pitch / variable helix
  • Vibration suppression at high RPM
  • Mirror-quality surface finish
Get Free Technical Advice
Module D — The Inspection

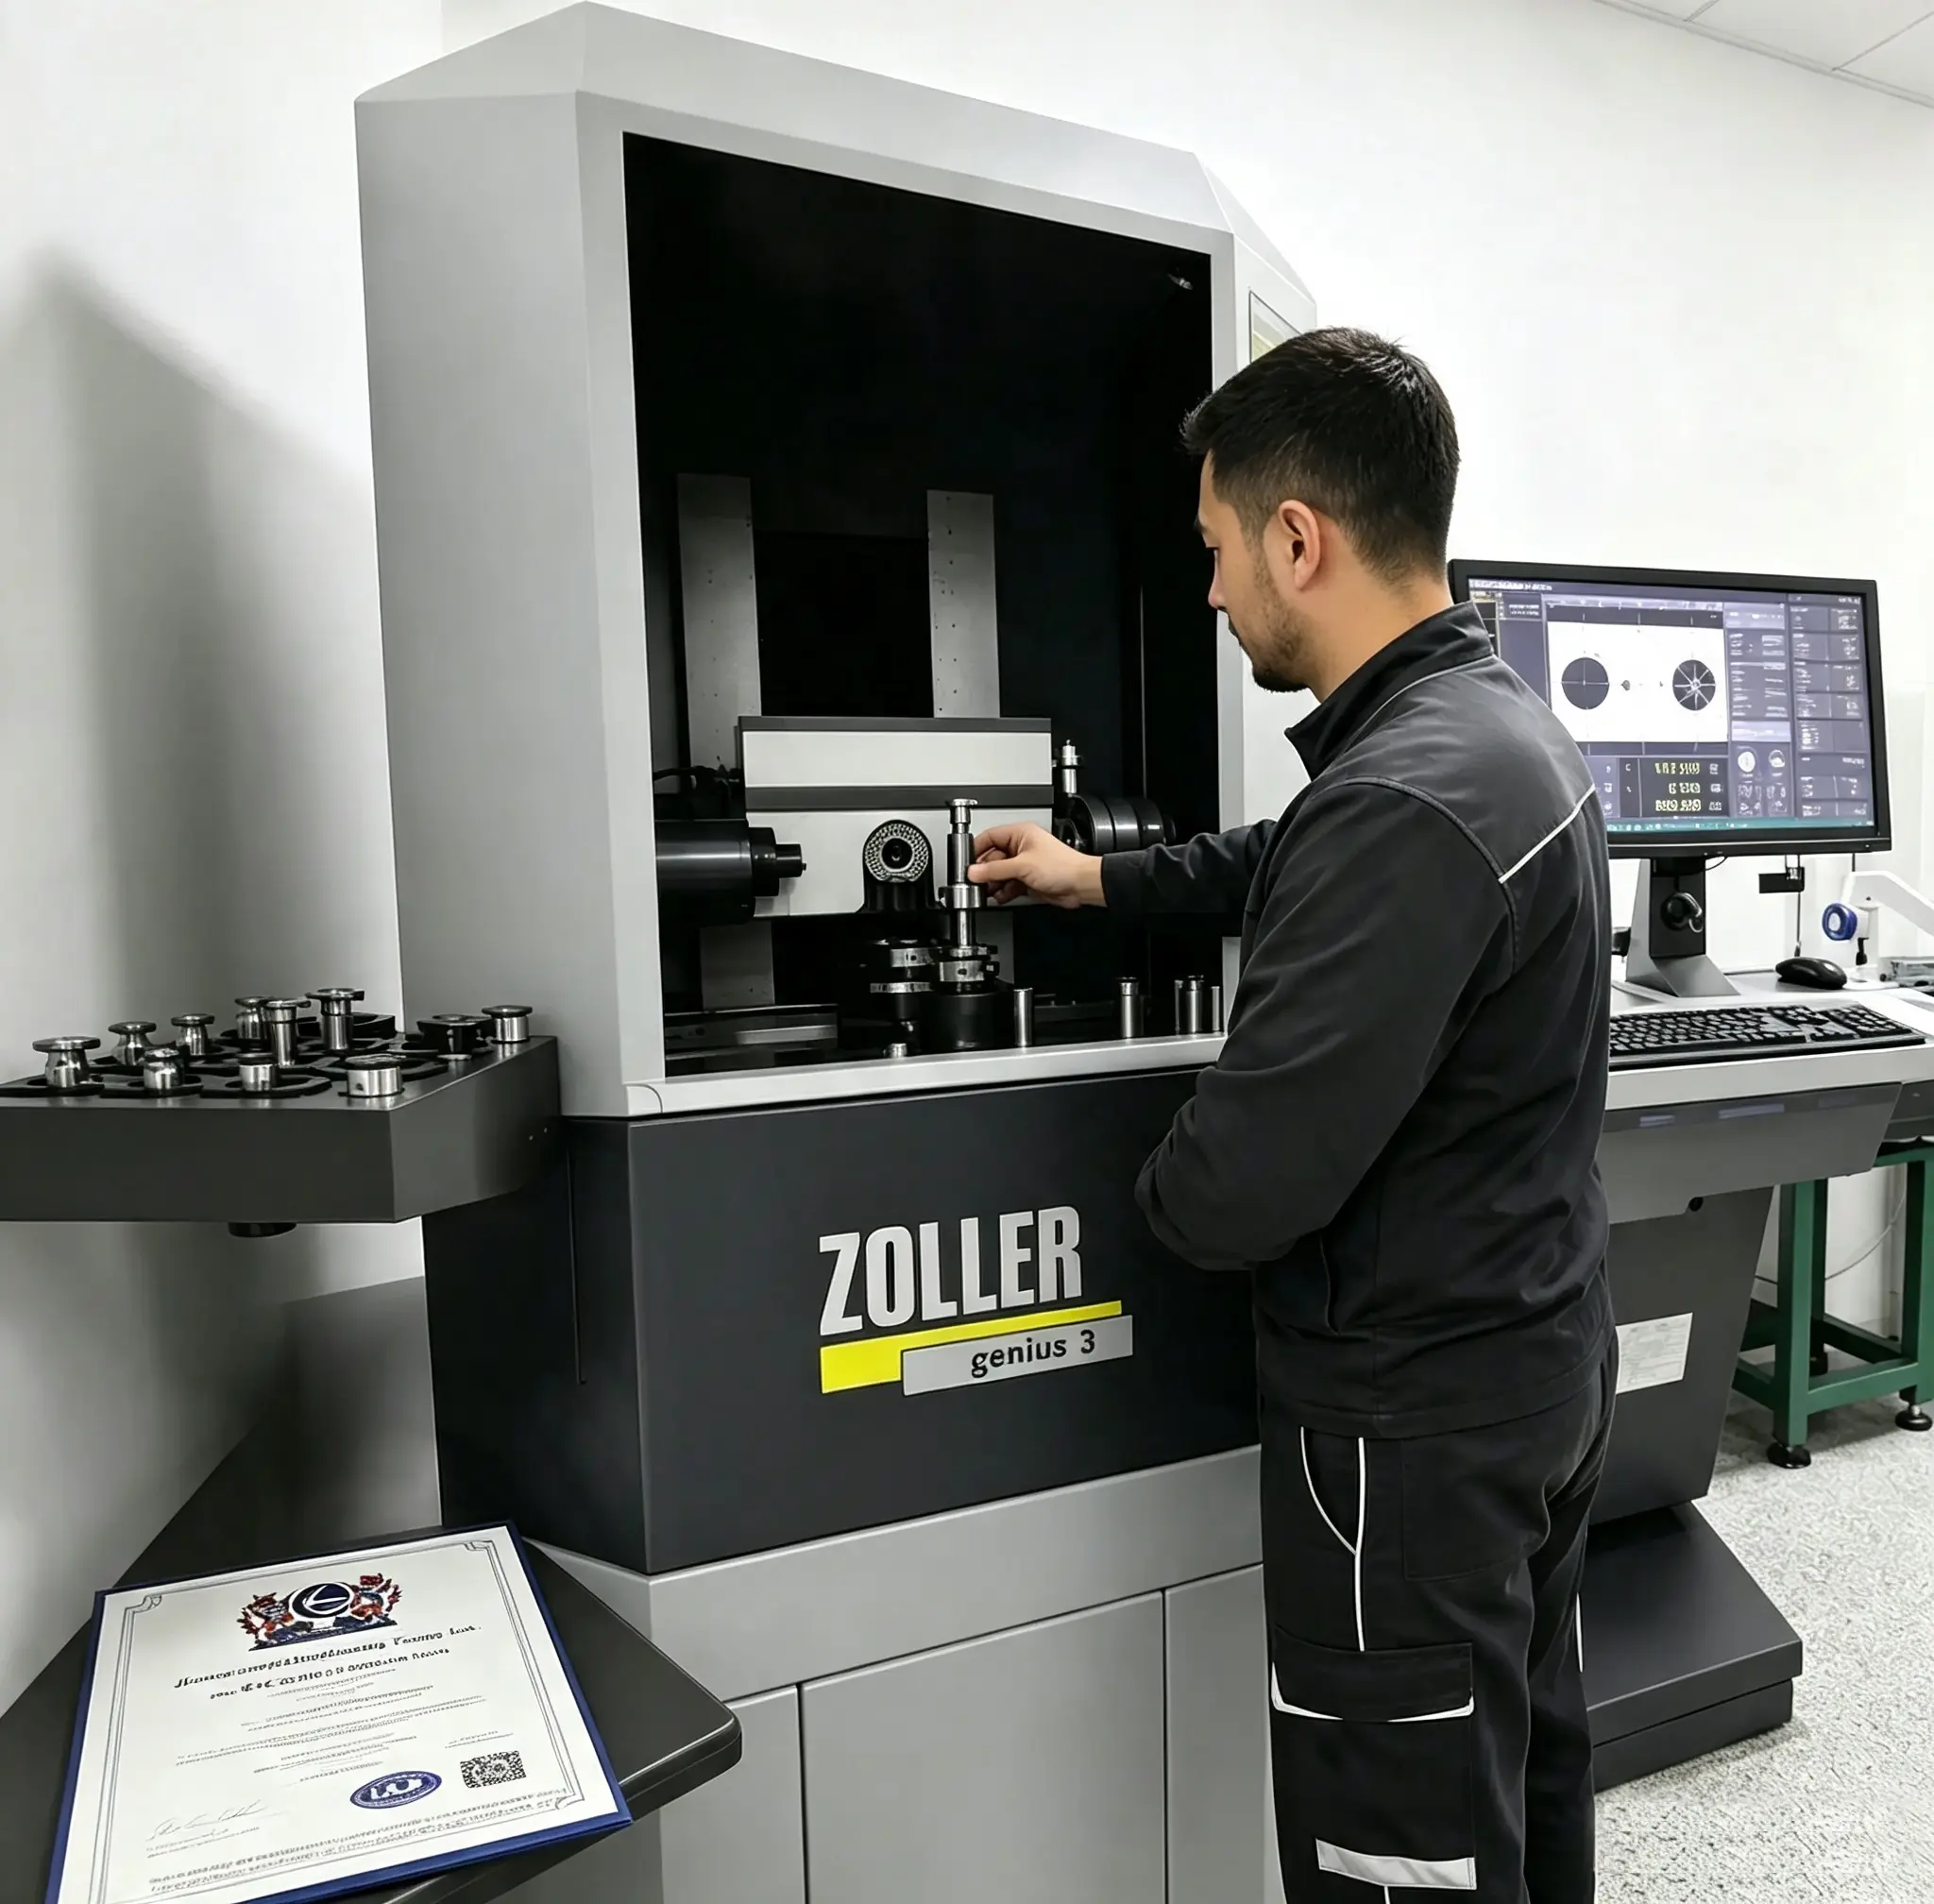
100% Zoller Precision Verification

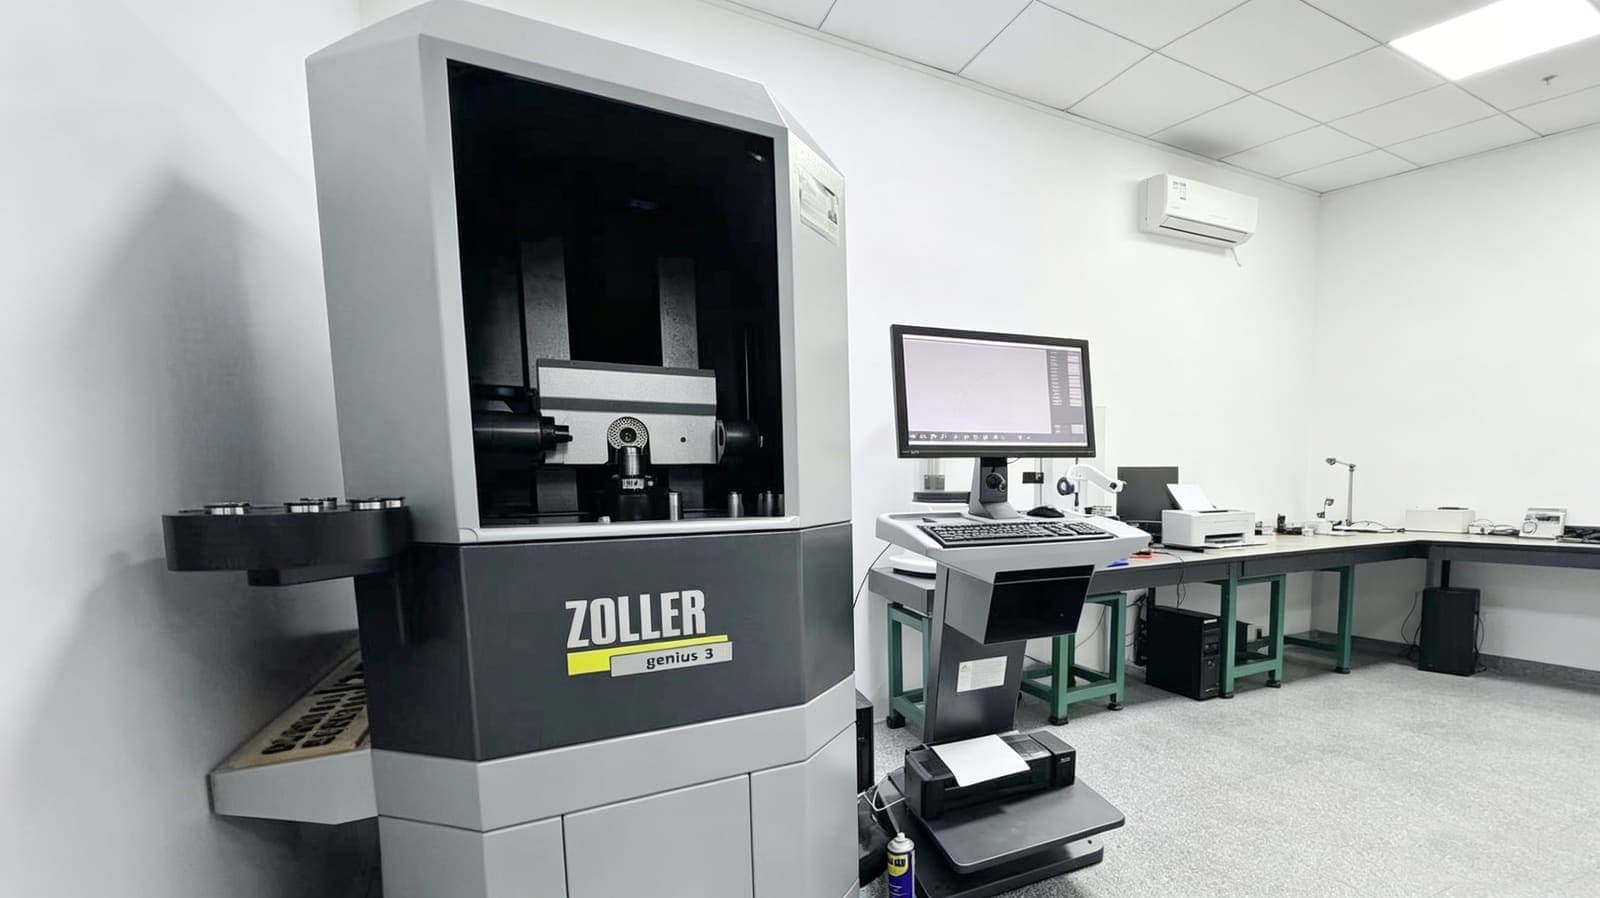
We don't leave quality to chance. Every single QT Tools end mill undergoes a rigorous 100% inspection process using the German Zoller Genius 3 measuring center. Our production base operates strictly under ISO 9001:2015 standards to guarantee micron-level consistency in every batch.

  • German Zoller Genius 3 technology
  • ISO 9001:2015 Certified Quality System
  • Micron-level edge & geometry control
Get Free Technical Advice
Module C · Anti-Vibration Geometry

Variable Helix Engineering: Eradicate Harmonic Chatter

The helix angle decides whether your machine sings or screams. Here is exactly why a generic 30° helix chatters — and how QT's variable helix geometry runs dead quiet at aggressive parameters.

Legacy Geometry

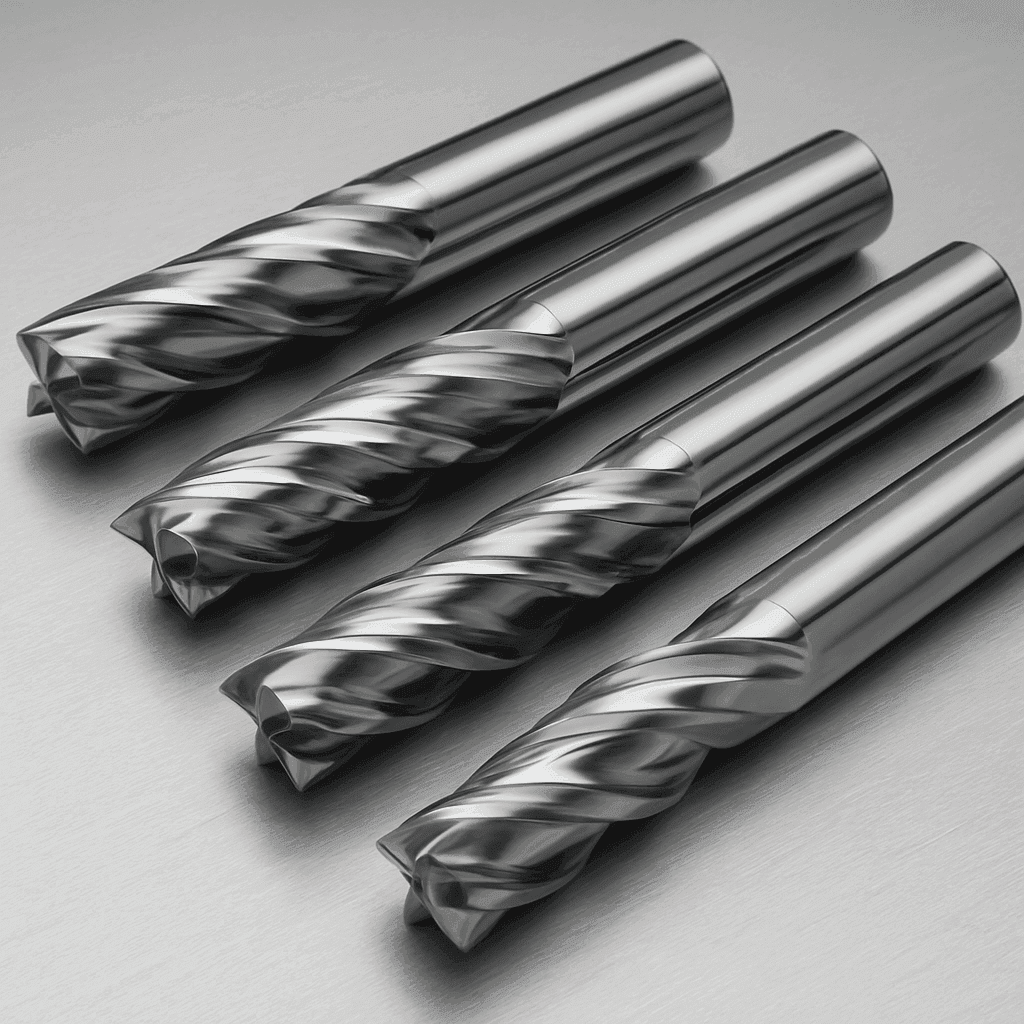
Standard 30° Helix (Generic Tools)

One fixed helix angle, one resonant frequency — the physics work against you the moment you push the feed.

  • Constant harmonics

    A single, uniform 30° helix resonates at one frequency — vibration reinforces itself instead of cancelling out.

  • Chatter marks

    At high spindle speeds the sidewall picks up visible chatter lines, forcing slower feeds and rework.

  • Corner chipping

    The cutting edge micro-fractures at the corner under dynamic load, killing tool life without warning.

  • Low Ap limit

    Unstable cutting caps your axial depth of cut, so every pocket needs more passes and more cycle time.
Recommended for Dynamic Milling / TPC

Industrial Grade

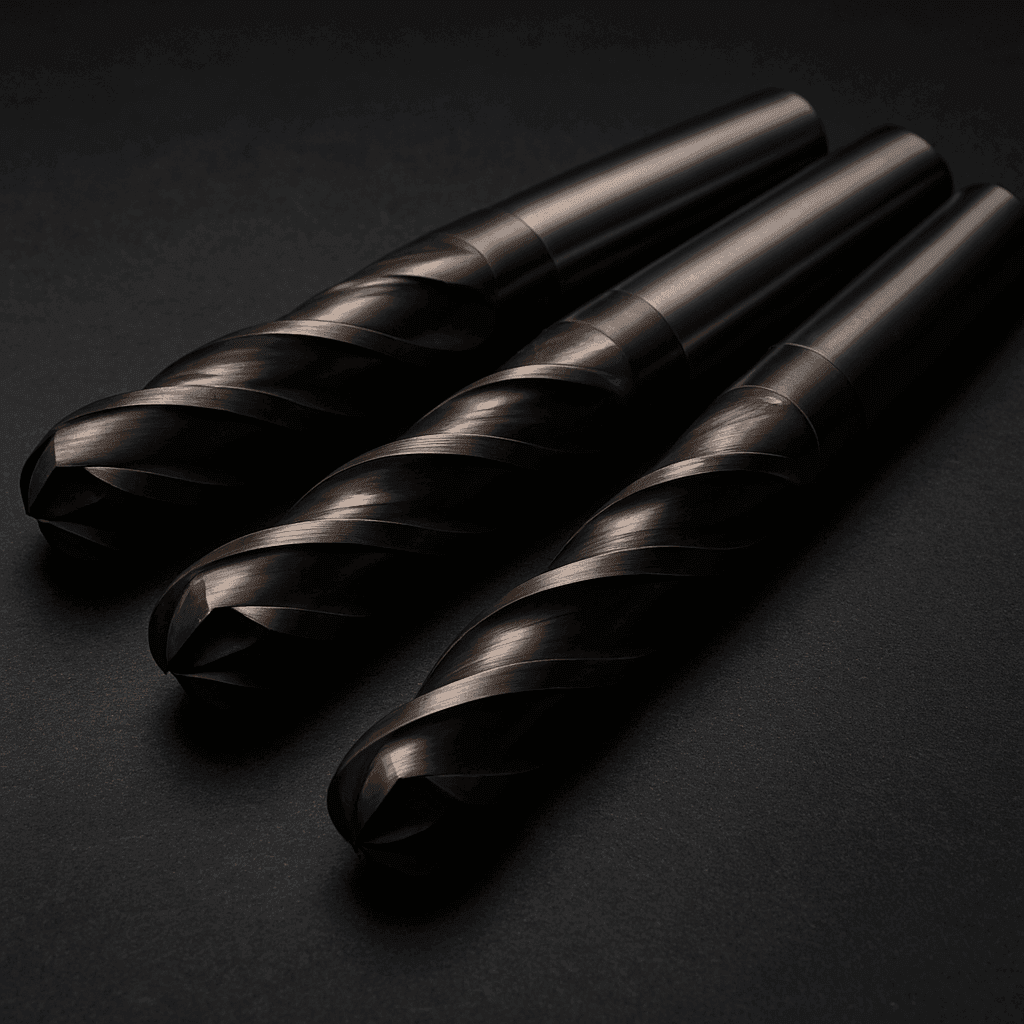
QT Variable Helix 35°/38° & 38°/41° (Industrial Grade)

Unequal, alternating helix angles break the vibration cycle before it can build — so you cut deeper, faster, and cleaner.

  • Disrupts resonance frequencies

    Variable 35°/38° & 38°/41° helix angles scramble the harmonic frequency — chatter is eliminated at the source, not damped.

  • 2× Axial Depth of Cut (Ap)

    Stable, chatter-free engagement lets you double axial Ap versus a generic helix, clearing material in far fewer passes.

  • Mirror Ra < 0.4μm

    Vibration-free sidewalls come off the machine at mirror-grade finish, cutting or eliminating secondary polishing.

Request Anti-Vibration Free Sample Tool

Tell us your material & machine — we'll match the exact helix spec for a free trial.

Custom Tooling & Extra Long Reach: 48–72H Production

Produzione Utensili Speciali in Metallo Duro · Sonderwerkzeuge nach Zeichnung

Custom Neck Relief (L1 Reach) Ground in 48–72 Hours

Solve deep-cavity reach and interference in mold & die machining. We grind custom neck relief (L1), step end mills, and extra-long shank tools from premium blank rods in 48–72 hours.

MOLD CAVITY CLEARANCE SCHEMATIC

d1Neck Diameter
Reduced diameter behind cutting edge to clear vertical mold walls.
L1Neck Relief Length
Custom ground to your exact pocket depth (e.g., 25mm, 45mm, 60mm).
lFlute Length
Kept short for maximum rigidity and zero chatter.
RCorner Radius
Optional R0.2 to R2.0 to reinforce tooth strength.
Guaranteed ConcentricityTIR < 0.003mmGerman Zoller Helicheck
  • Zero Toolholder Interference

    Eliminates ER collet nut and shrink-fit toolholder contact against steep draft angles and deep ribs.

  • 48 to 72 Hours Fast Turnaround

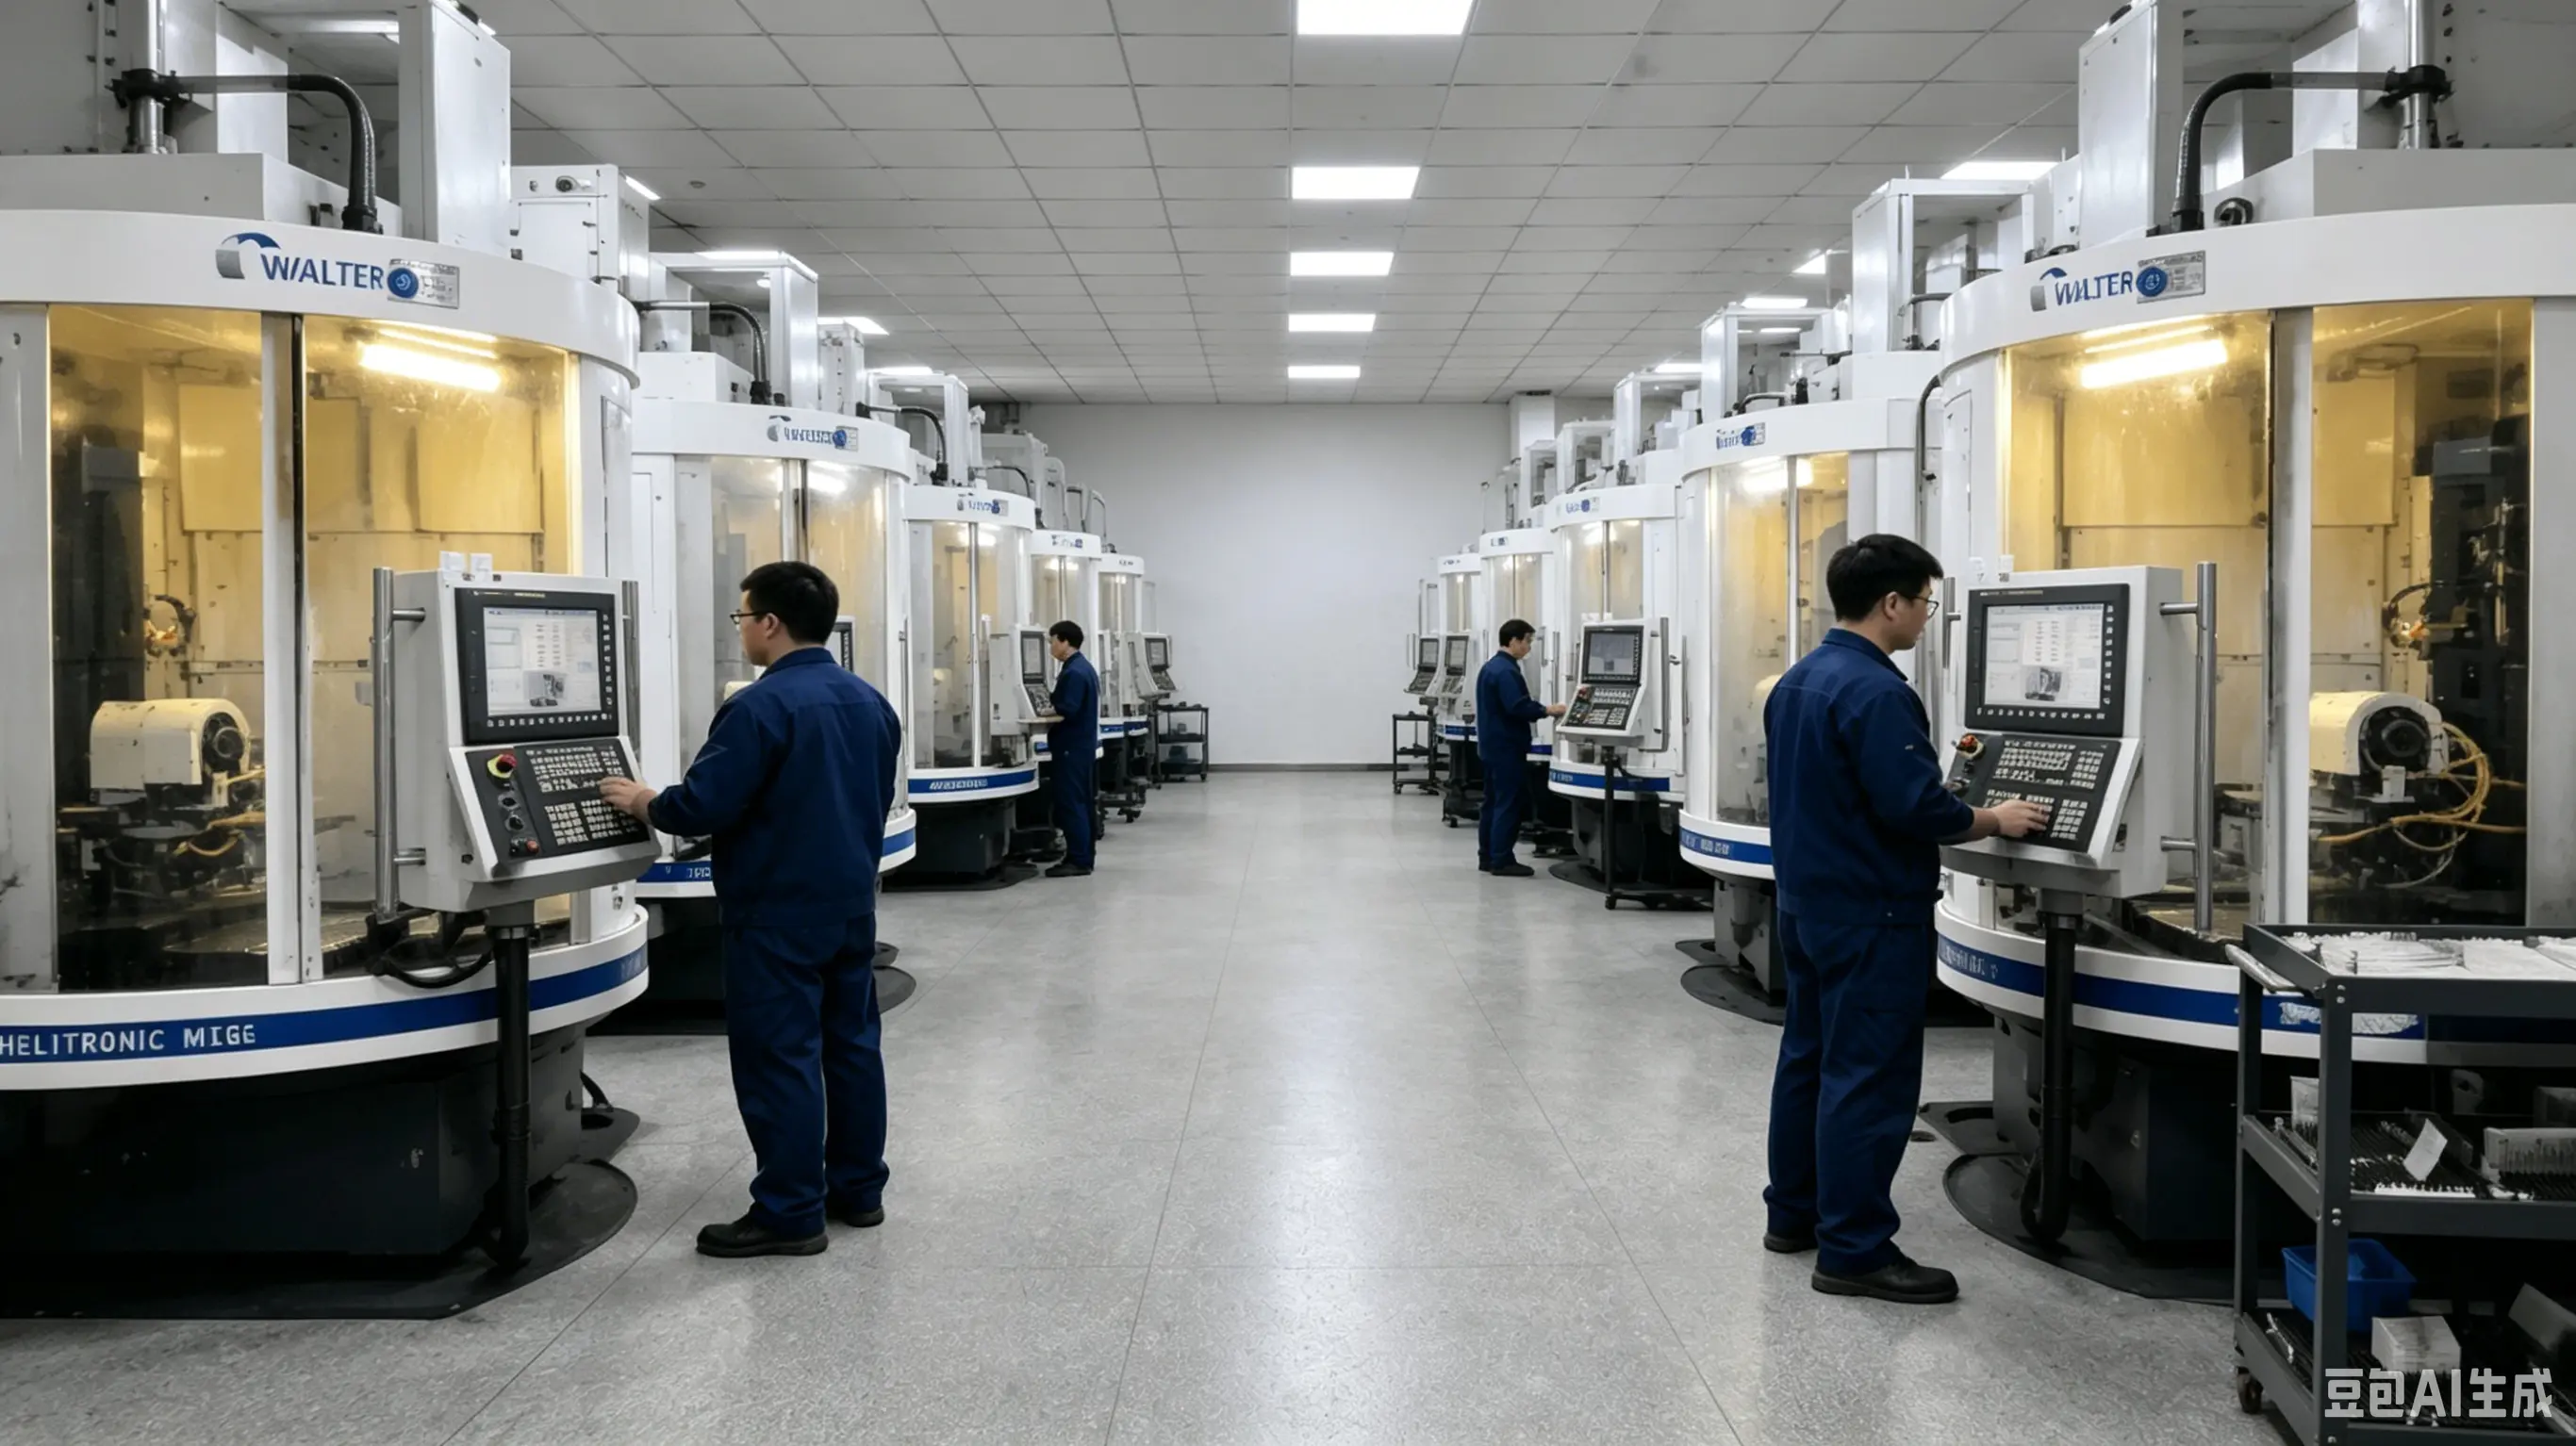
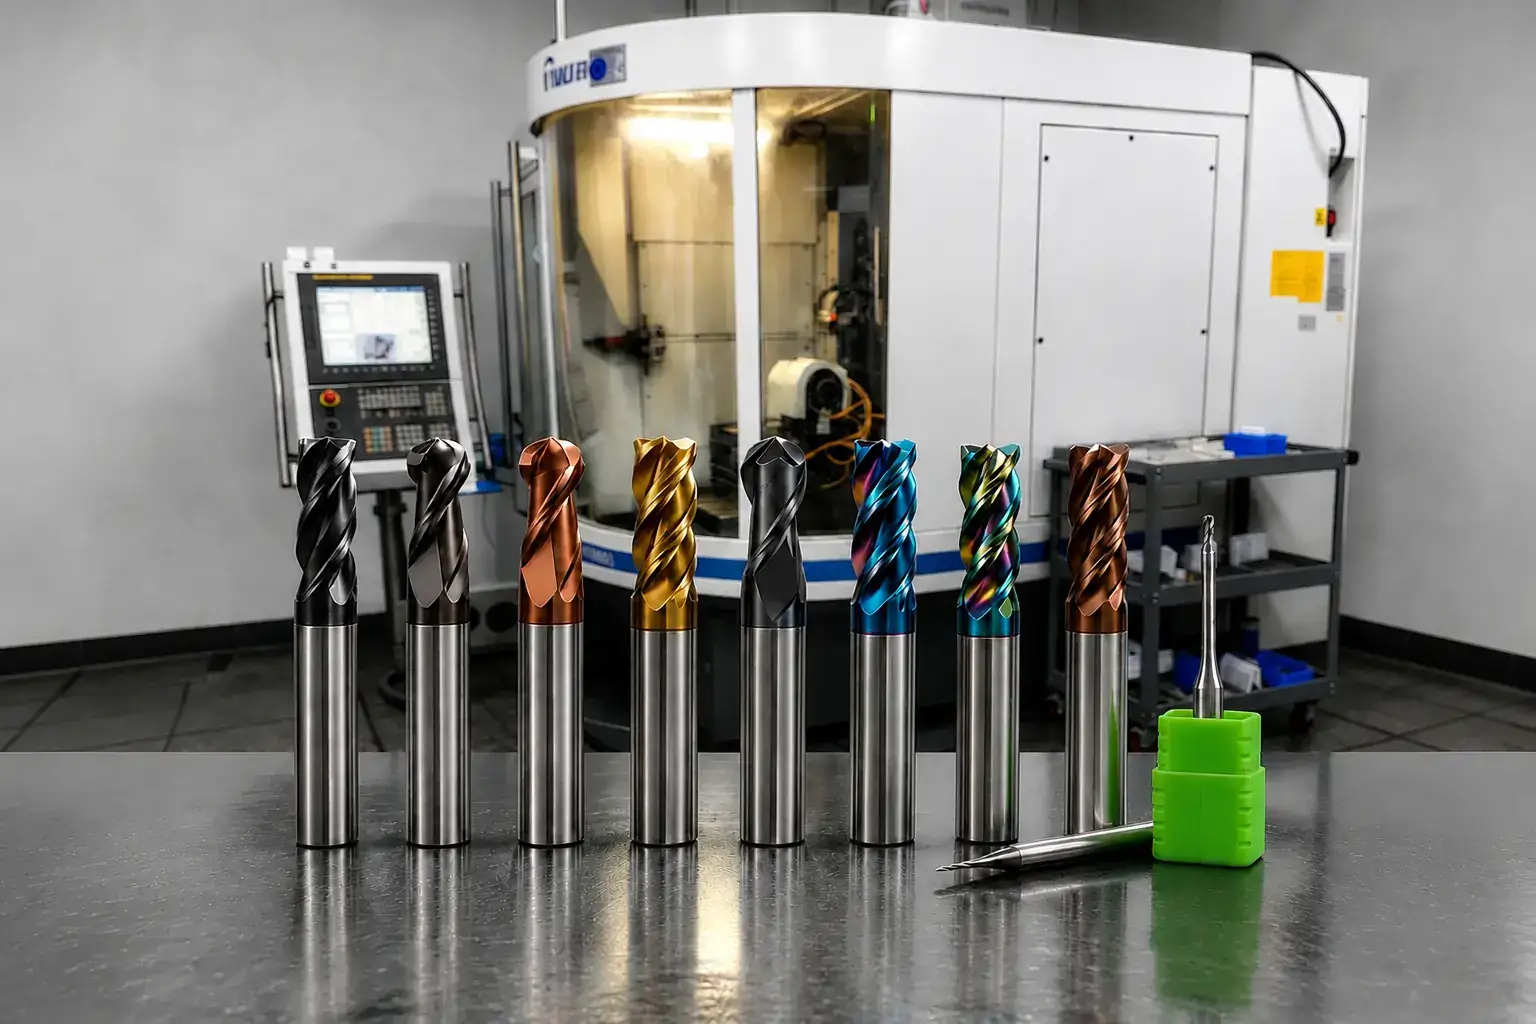
    50+ Walter and Rollomatic 5-axis grinders with flexible production scheduling. We grind directly from blank rods, with no 6-week European backlogs.

  • Direct Drawing Assessment

    Send STEP, DXF, or a simple 2D sketch. Our application engineers confirm parameters and toolpath rigidity within 2 hours.

Extra Long Reach Metric Matrix

Diameter × Overall Length (OAL)

  • D6
  • D8
  • D10
  • D12

Reinforced tapered core for 35% higher rigidity against bending deflection during deep pocket milling.

100% Material Traceability: Zero Bait-and-Switch Policy

Substrate Transparency: You Get Exactly What You Pay For

Overseas machine shops fear uncertified recycled scrap masquerading as virgin carbide. At QT Tools, we operate on complete engineering honesty: choose between imported European rods, our certified 100% virgin domestic flagship series, or value-engineered job-shop substrates—clearly declared, batch-inspected, and never mixed.

AEROSPACE & HRC 55-65

Pro-Mold European Substrate

Grain Size
Ultra-fine 0.2–0.4μm sub-micron
Cobalt Content
12% Co for extreme shock resistance
Application
Hard milling tool steels (H13, SKD11, D2, S136) up to HRC 65, Titanium, and Inconel
Origin
100% Virgin European / German carbide rod sourcing
Inquire European Substrate
90% Performance @ 40% Cost
100% PURE VIRGIN DOMESTIC

Flagship Industrial Series

Grain Size
0.6–0.8μm micro-grain carbide
Guaranteed Strength
Transverse Rupture Strength (TRS) > 3,800 MPa
Zero Scrap Policy
100% primary smelter domestic tungsten carbide, absolute zero recycled content
Application
Production milling in Stainless Steel (304/316), Pre-hardened Steel (P20/718), Cast Iron, and Aluminum
Check Flagship Pricing
VALUE-ENGINEERED JOB SHOP

Commercial Utility Series

Honest Declaration
Built for low-speed CNCs, manual milling, structural mild steel, and disposable high-abrasion roughing
Strict Principle
Commercial substrates priced transparently. We never mislabel or mark up utility grades as virgin carbide
Target
High-volume distributors and price-sensitive commercial users seeking honest factory pricing
Inquire Commercial Batch

OEM Substrate Freedom: Sourced to Your Exact Blueprint

Need private label branding or designated carbide rod brands? With 50+ German Walter & Swiss Rollomatic 5-axis grinding centers, we support flexible toll-grinding and custom material specifications.

Consult Tooling Engineer on WhatsApp
Harmonic Suppression & Cycle Time Reduction

Stop Chatter Screeching & Slow 3D Scanning

Engineered for shop-floor productivity: break harmonic resonance on thin-wall stainless steel with unequal helix geometries, and replace slow 3D ball-nose deburring with single-pass convex radius form cutters.

CHATTER-FREE ALTERNATIVE

38°/41° Unequal Helix & Variable Flute Spacing

38°/41° Unequal Helix & Variable Flute Spacing: Engineered to break natural harmonic frequencies during heavy-feed side milling and full-slotting. Eliminates chatter marks and delivers VariMill-grade surface finishes at 40% of the cost.

Substrate
100% Virgin European Sub-Micron Rod (0.4μm, 12% Co).
Thermal Barrier
TiAlSiN Nano-Composite Coating resists heat up to 1,100°C — eliminates Built-Up Edge (BUE) in 304, 316, and Duplex Stainless.
Center-Cutting
100% axial center cutting geometry for vertical plunging and steep helical ramping without pilot holes.
Runout Guarantee
TIR < 0.003mm verified on German Zoller Helicheck.
Request Anti-Chatter Speeds & Feeds
SINGLE-PASS EDGE PROFILING

Corner Rounding / External Radius Cutters (R0.5–R6.0)

Corner Rounding / External Radius Cutters (R0.5 to R6.0): Single-pass precision edge radiusing for mold plates and aerospace frames. Eliminates slow 3D ball-nose profiling and reduces edge-deburring cycle time by 80%.

Stocked Radii
R0.5, R1.0, R1.5, R2.0, R2.5, R3.0, R4.0, R5.0, R6.0 in stock.
Relieved Design
Symmetrical dual-relieved profile prevents secondary edge binding on vertical cavity walls.
Cycle Time Reduction
Eliminates 10+ minutes of 3D CAM step-down rastering down to a 10-second contour pass.
Applicable Metals
Mold steels (P20, NAK80, H13), 6061/7075 Aluminum, Cast Iron, and Stainless Steel.
Check External Radius Stock & Pricing

All tools ground on 50+ German Walter & Swiss Rollomatic 5-axis CNC grinding centers. Certified runout TIR < 0.003mm.

The Solution

One series engineered for each job

No 500-page catalog to wade through. Pick your material, and we match you to the line built to dominate it.

Polished uncoated carbide end mills with high-helix flutes for aluminumChat about the The Aluminum King on WhatsApp
⚡ 3-FLUTE MIRROR-POLISHED | 45° HIGH HELIX3-Flute · Large Helix

The Aluminum King

High-Speed Aluminum Machining (Fresas de Carburo para Aluminio)

3-Flute Mirror-Polished Flutes (Ra < 0.1μm) + 45° High Helix: Zero chip packing during 24,000 RPM high-speed machining.

Specifically engineered for 6061-T6, 7075 aerospace aluminum, and copper. Ultra-smooth micro-ground flute troughs completely eliminate chip welding and built-up edge (BUE), allowing aggressive high-feed slotting and mirror wall finishes.

Fresas para aluminio diseñadas para evitar la adherencia del aluminio a altas RPM. Acabado espejo Ra < 0.1μm.

Custom Solutions & OEM Available

We produce non-standard geometries and imperial sizes to your exact drawings. Send us a print — we'll engineer the tool.

Send Your Drawing
1,000+ STANDARD SKUS IN STOCK | 48H DISPATCH

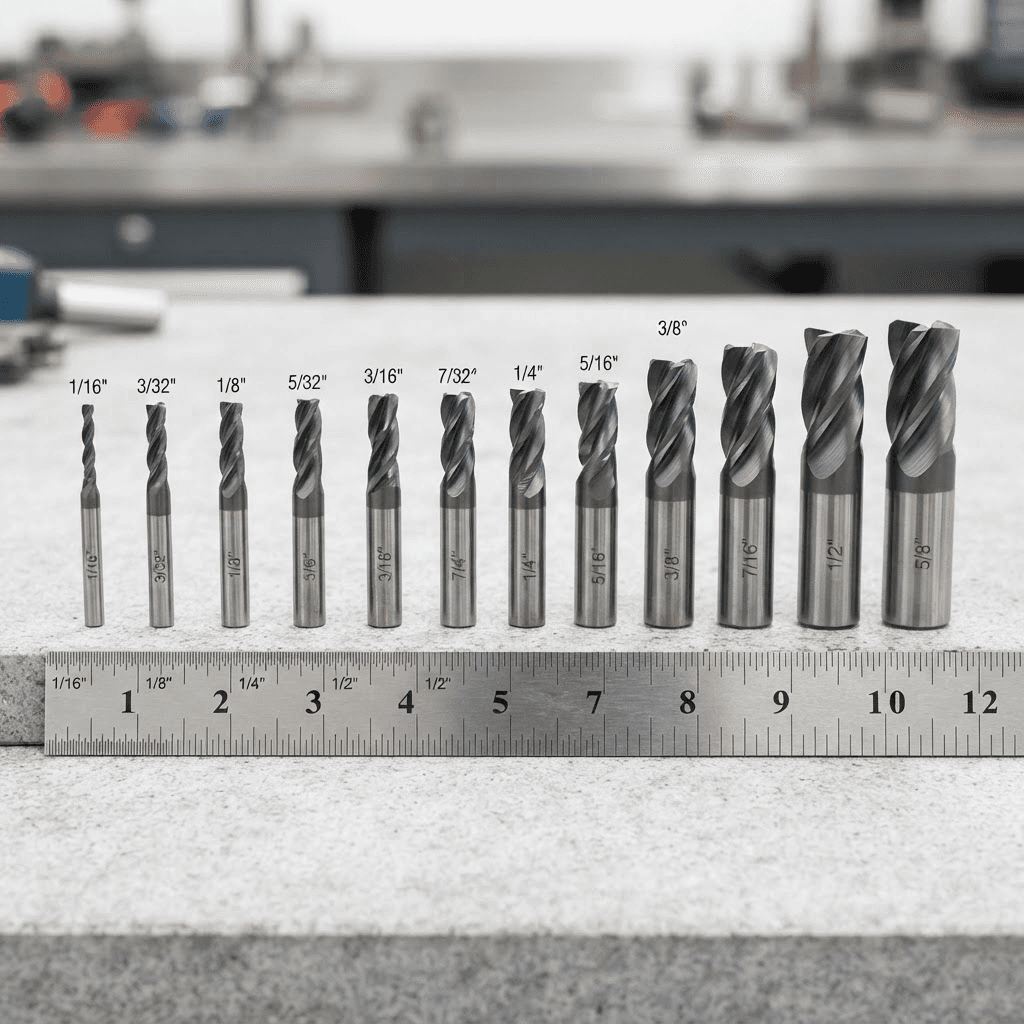
Popular Sizes Quick Reference

Tap any row below to check stock availability, request custom neck relief length, or get instant WhatsApp pricing.

Popular carbide end mill sizes with recommended flute count, coating, application material, and a WhatsApp price and stock inquiry link for each size.
DiameterFluteCoatingApplicationAction
Ø0.5 mm2-FluteAlTiN (Ultra-Fine)Micro engraving & electrodesCheck Price & Stock
Ø1 mm2-FlutenACo-Blue (Nano)Micro hardened steel HRC55+Check Price & Stock
Ø2 mm2-FluteAlTiN (Ultra-Fine)Micro slotting & fine detailCheck Price & Stock
Ø4 mm4-FlutenACo-Blue (Nano)Hardened steel HRC55-65Check Price & Stock
Ø6 mm3-FluteDLC (Diamond-Like)Aluminum & non-ferrousCheck Price & Stock
Ø8 mm4-FluteAlCrN (Nano-Composite)Stainless SUS304 / 316Check Price & Stock
Ø10 mm4-FlutenACo-Blue (Nano)Mold & die roughingCheck Price & Stock
Ø12 mm4-FluteAlCrN (Heat-Resistant)Titanium & InconelCheck Price & Stock
Ø16 mm5-FluteAlCrN (Nano-Composite)High-feed finishingCheck Price & Stock
1/8"4-FluteAlTiN (Ultra-Fine)Inch-series general steelCheck Price & Stock
1/4"3-FluteDLC (Diamond-Like)Inch-series aluminumCheck Price & Stock
1/2"4-FluteAlCrN (Nano-Composite)Inch-series stainless & alloyCheck Price & Stock
The Proof

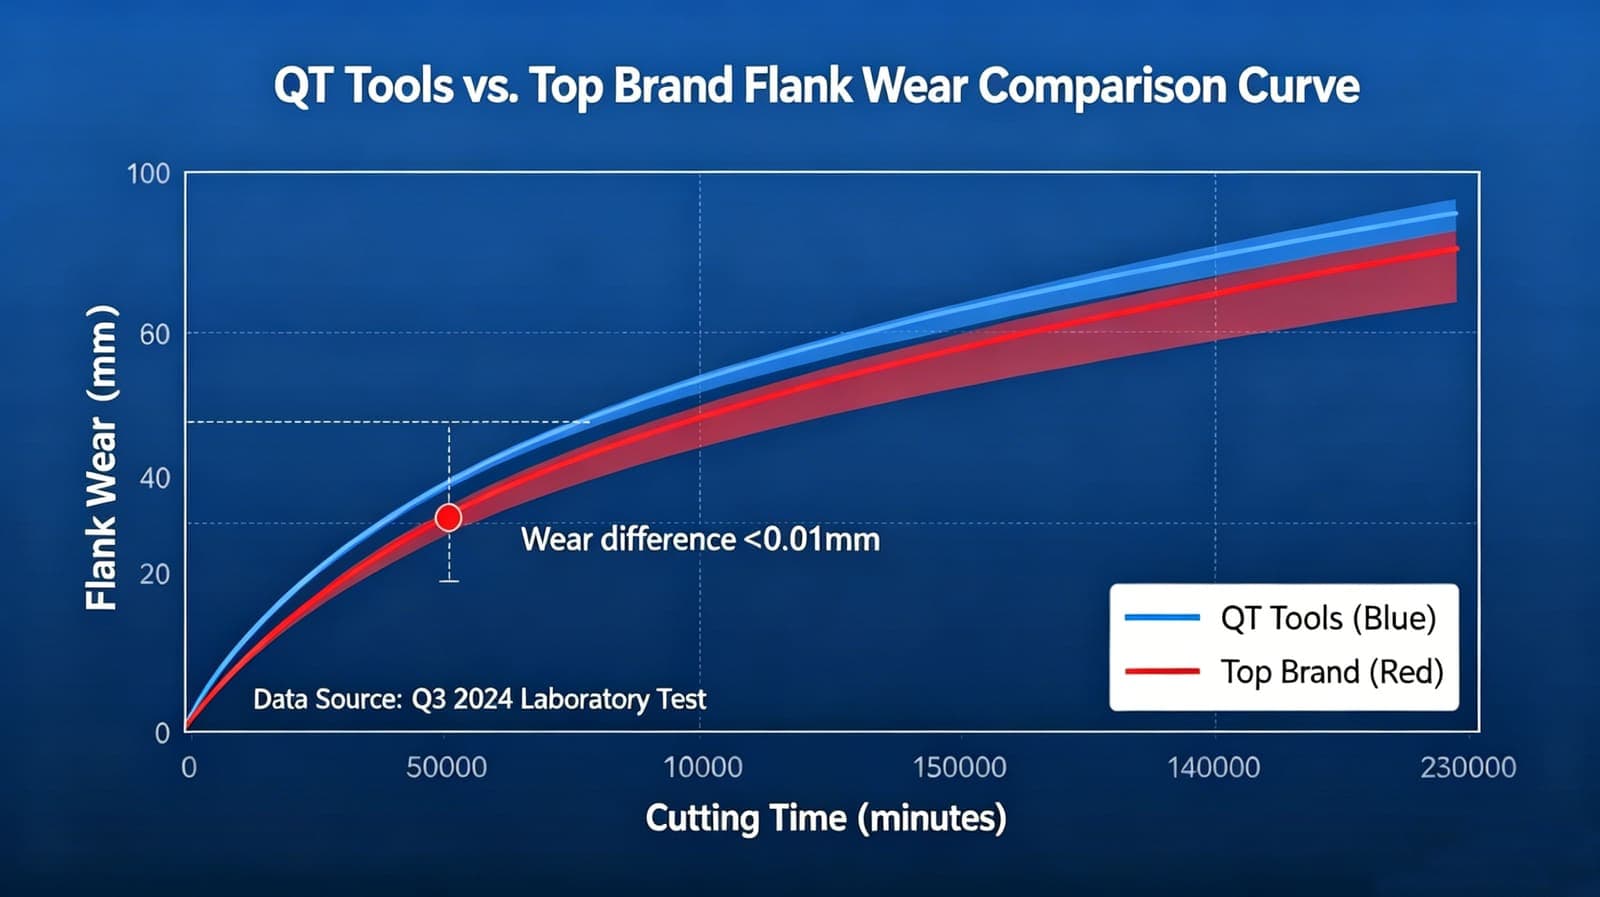
Flank wear that tracks the A-brands

Milling P20 mold steel at HRC52, identical speeds and feeds. We measured how many parts each tool produced before reaching 0.2mm flank wear. QT Tools tracks right alongside the leading international brand — at a fraction of the cost.

“We don't just sell tools; we manage precision down to the micron.”
0.18mm
Flank wear after 1,000 parts
+162%
Tool life vs. generic mills
≤ 2 wk
Typical production lead time
Flank wear comparison curve showing QT Tools (blue) tracking the top international brand (red) with a wear difference under 0.01mm

Internal benchmark, P20 @ HRC52. Actual results vary by machine, setup, and parameters.

The Authority

We manage precision down to the micron

Switching suppliers is a real risk. Here is the hard proof that QT Tools is a genuine Chinese manufacturer with German-grade production — not a reseller.

Rows of Walter Helitronic 5-axis CNC tool grinding machines operated by technicians on the QT Tools grinding floor in Changzhou, ChinaGrinding floor · Changzhou, China
Zoller genius 3 optical tool measuring machine in the QT Tools micron-level QC labQC lab · Micron-level inspection

100% Walter 5-axis grinding

Every tool is produced on Walter (Germany) 5-axis CNC grinding machines. You buy direct from the people who make the chips — not a trading desk reselling someone else's lots.

100% Zoller inspection

Every tool is verified on Zoller (Germany) measuring centers to micron tolerance. Diameter, runout, and edge prep are checked before it ever ships.

Exporting to 30+ countries

We supply mold makers and CNC shops across Europe, North America, and Southeast Asia, with full export documentation and stable QC.

Equipment & capabilities

  • Walter (Germany) 5-axis CNC tool grinding
  • Zoller (Germany) optical measurement & inspection reports
  • PVD coating line — AlTiN / TiSiN / nACo
  • Full material traceability per batch
Global Success Stories

Trusted by 500+ Machining Partners Worldwide

  • Verified Customer
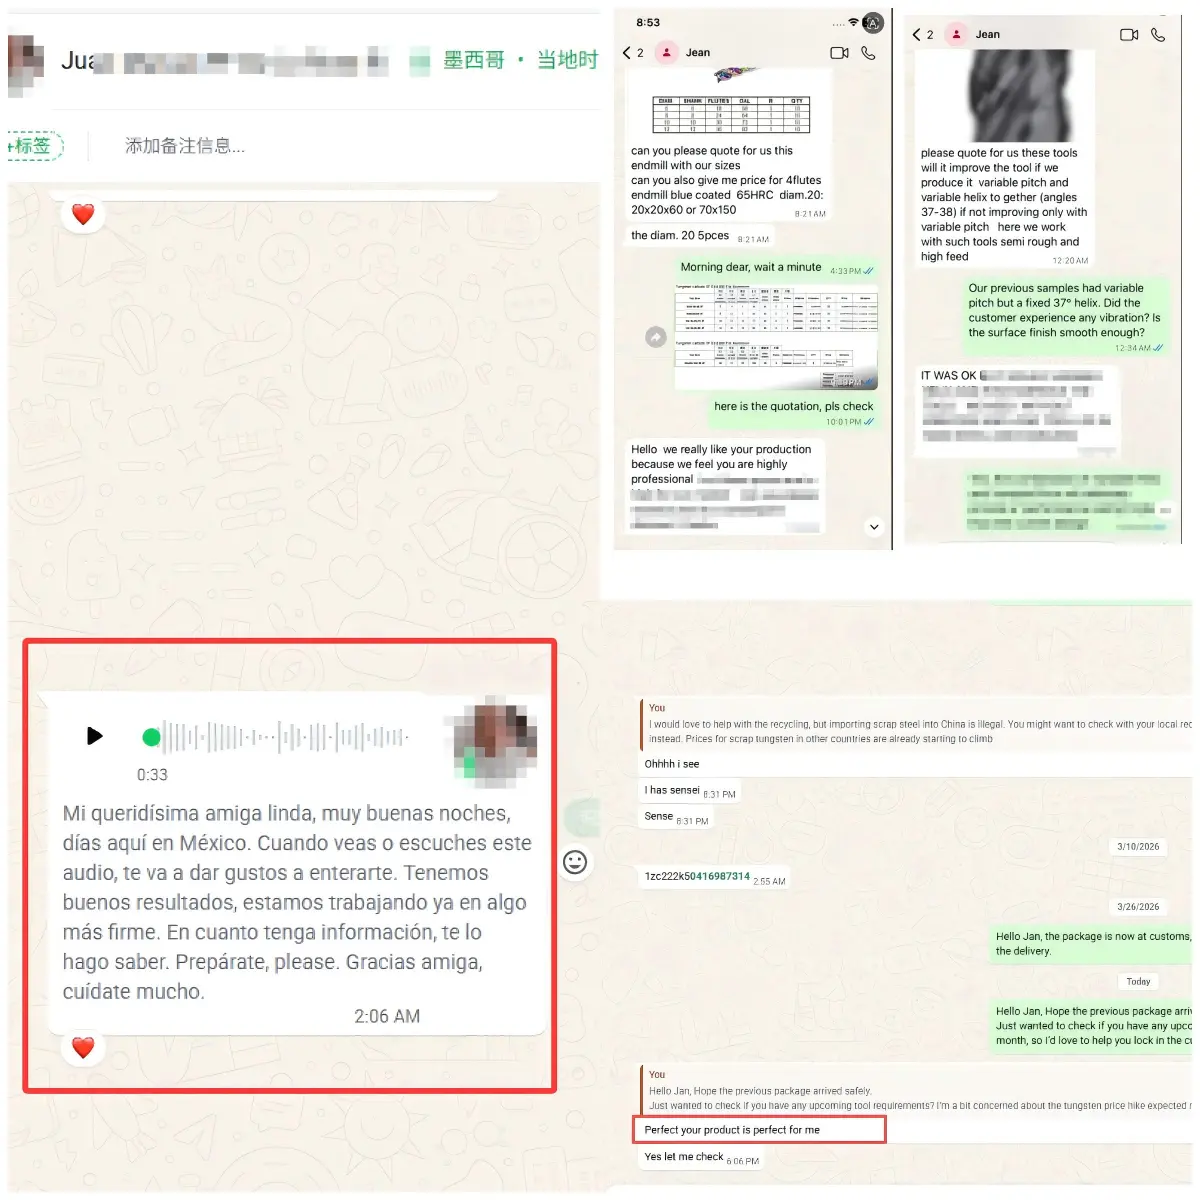
    “We really like your production because we feel you are highly professional.”

    Original feedback from WhatsApp business chat.

    Jean
    Procurement Buyer
  • Verified Customer
    “We have good results with the samples. Working on a firmer order now.”

    Original feedback from WhatsApp business chat.

    Juan
    Workshop Owner
    Mexico
  • Verified Customer
    “Perfect, your product is perfect for me.”

    Original feedback from WhatsApp business chat.

    Jan
    CNC Machinist
    Venezuela

Real Conversations, Real Trust.

See what our partners are saying about QT Tools on WhatsApp.

Collage of verified WhatsApp business chats with QT Tools customers discussing carbide end mill quotes, samples, and orders

Join 500+ satisfied partners. Chat with an Engineer Now

Ask the Engineers

Technical FAQ: Everything You Need to Know

Straight answers on precision, hardened-steel performance, cost, and lead times—written by the people who grind the tools.

Loading...